The Mud King — Making transformation less of a royal mess.
Agentic AI · Manufacturing
Agentic AI on the factory floorAgents, knee-deep in the plant
Factories already have the data: sensors, SCADA, MES, ERP. What they lack is someone who acts on it in time. I built the Digital Factory Console to show what changes when an agent makes that call, inside the controls a plant needs.Your plant already knows the lot is bad. The camera said so six times. This is what happens when something finally listens.
A simulated plant with illustrative numbers, not a client system. Every visitor shares the same plant, and it resets daily. The console is in English.
Same defect, two lines
The lot that ships, and the lot that stays.Six alarms. One shipment. Four hours of regret.
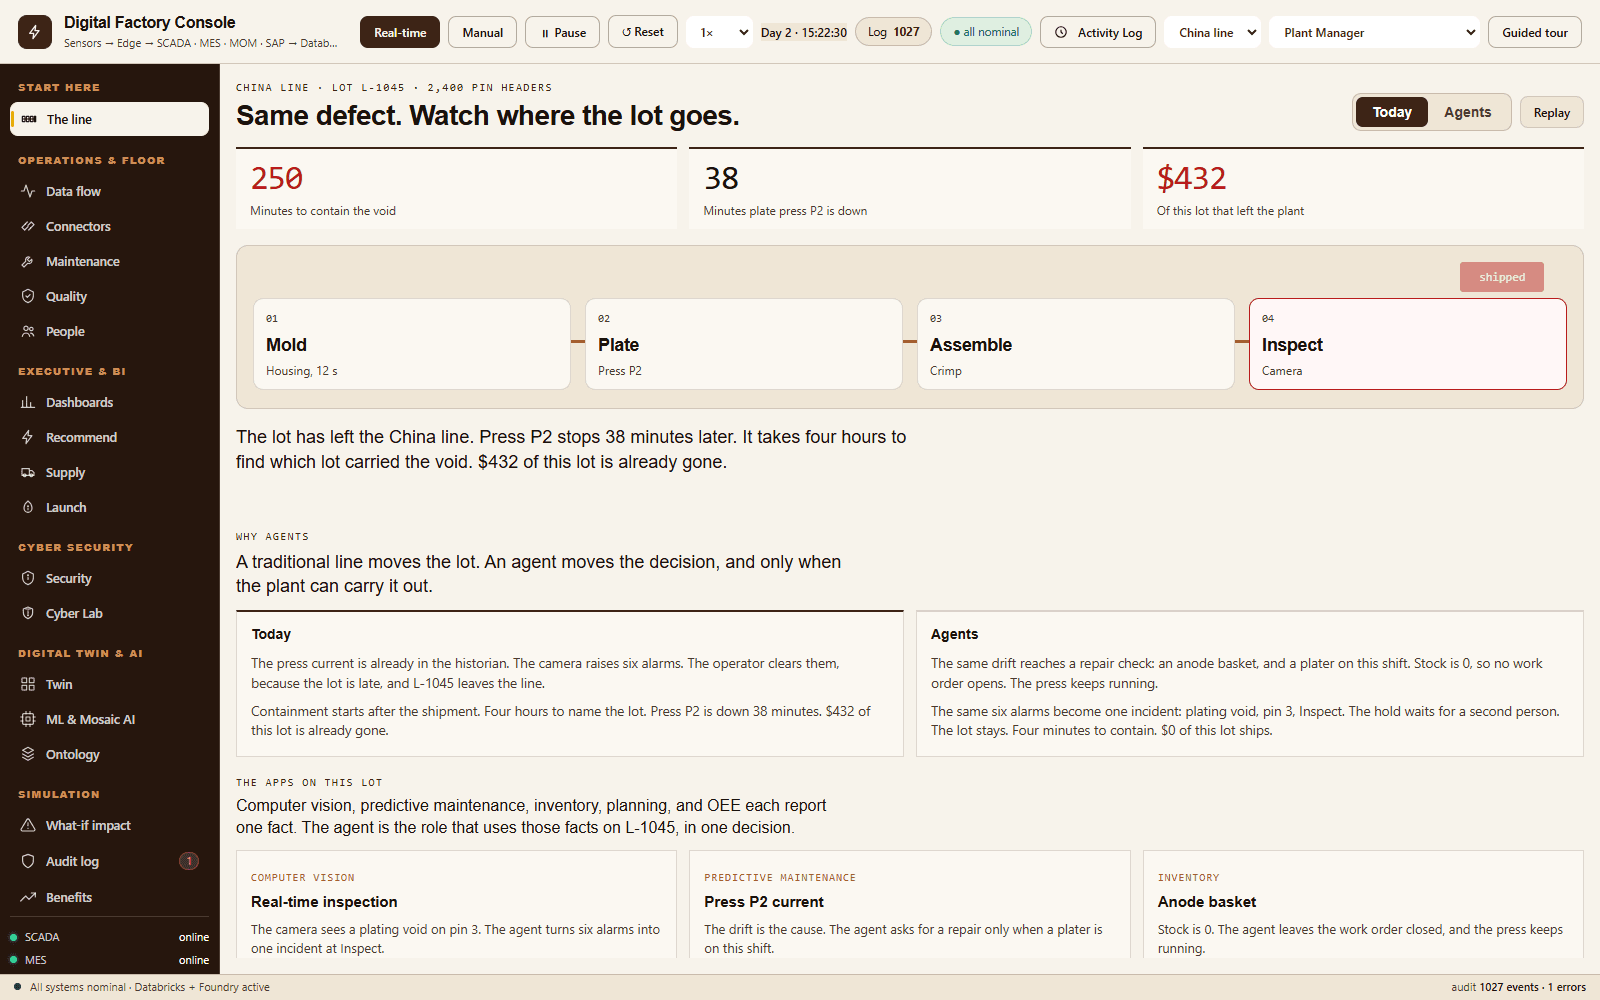
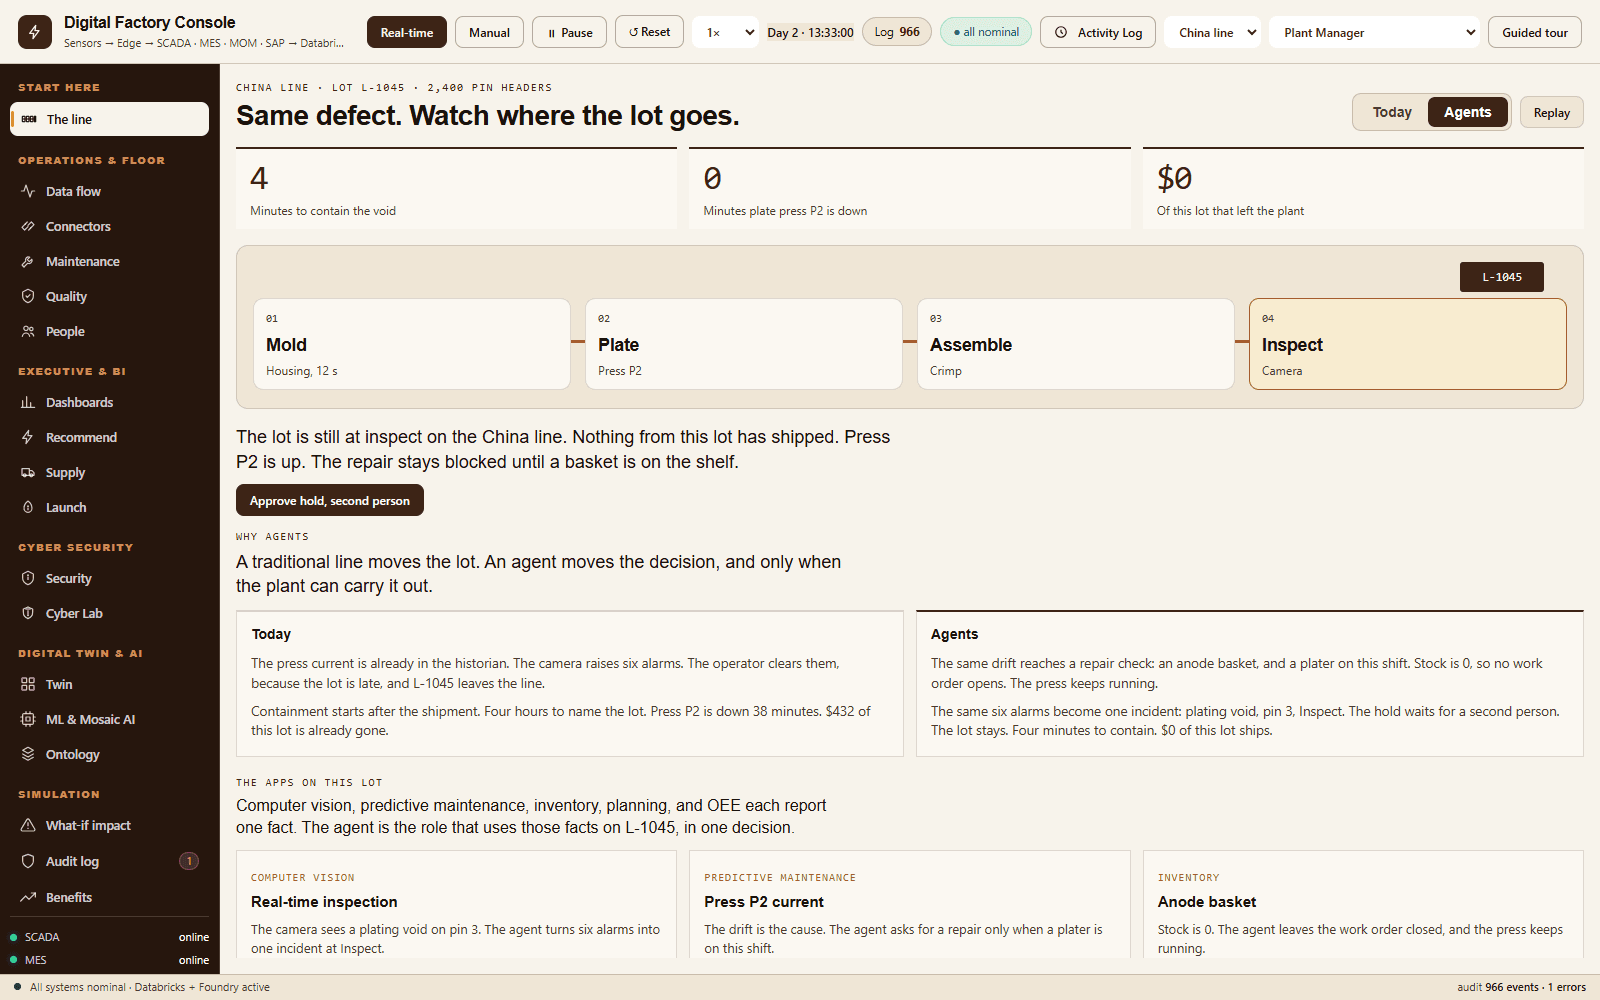
The console’s first screen runs one plating defect on lot L-1045, 2,400 pin headers on a China line, twice: once as most lines run today, once with agents. The figures are the simulation’s.
Today
minutes to contain the defect
250
minutes plate press P2 is down
38
of this lot left the plant
$432
The press current is already in the historian. The camera raises six alarms. The operator clears them, because the lot is late, and L-1045 leaves the line. Containment starts after the shipment.
With agents
minutes to contain the defect
4
minutes plate press P2 is down
0
of this lot left the plant
$0
The same drift reaches a repair check: an anode basket, and a plater on this shift. Stock is zero, so no work order opens and the press keeps running. The six alarms become one incident at Inspect. The agent drafts a hold, a second person approves it, and the lot stays.
Where the agent sits
The apps report facts. The agent decides.Five dashboards, zero decisions. Until now.
Computer vision, predictive maintenance, inventory, planning and OEE each report one fact. The agent is the role that uses those facts on one lot, in one decision.
Computer vision
The camera sees a plating void on pin 3.
→ Turns six alarms into one incident at Inspect.
Predictive maintenance
Press P2’s current is drifting. The drift is the cause.
→ Asks for a repair only when a plater is on this shift.
Inventory
The anode basket the repair needs is out of stock.
→ Leaves the work order closed, so the press keeps running.
Planning
The lot is late, and the schedule wants it out the door.
→ Holds it at Inspect, so the defect is settled first.
OEE
Press P2 is the line’s constraint.
→ Keeps its downtime at zero while the repair cannot be done.
Closed-loop quality
A hold stops the lot, and a release lets it go.
→ Drafts the hold. A second person approves it, and release uses the same rule.
The digital thread underneath
An agent is only as good as the plumbing.No pipes, no agent.
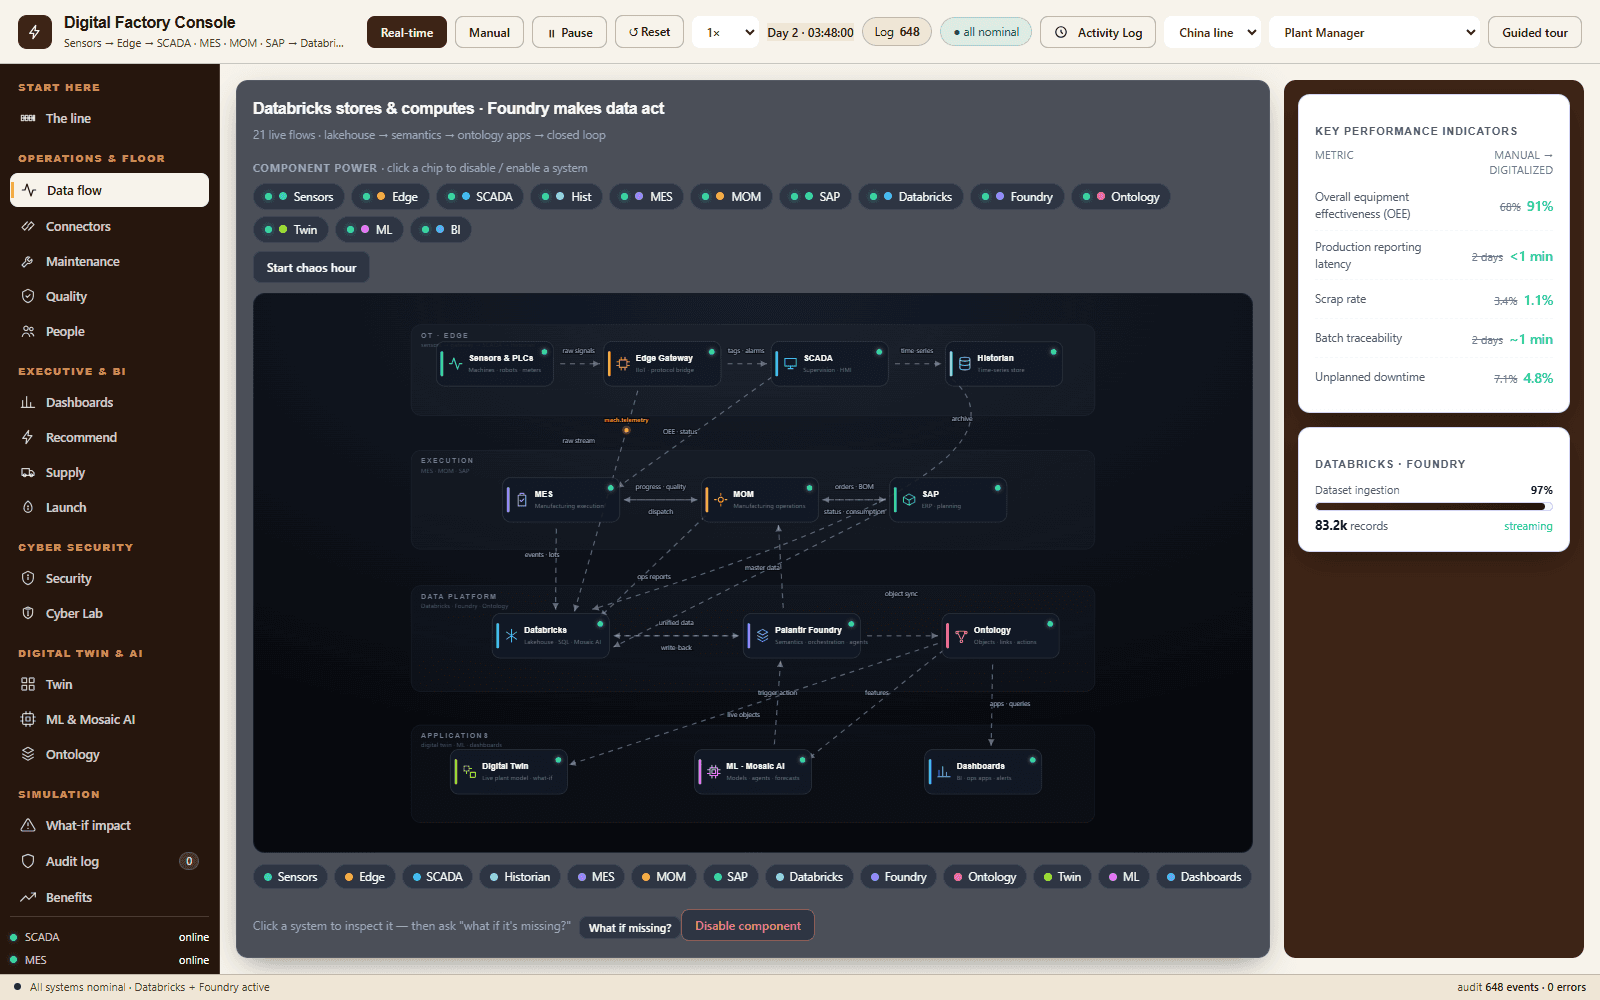
Agents cannot act on data that never leaves the machine. Behind the line screen, the console runs the full stack, 13 systems and 21 live data flows, and lets you switch any system off to see what breaks.
01
Shop floor and edge
Sensors and PLCs, edge gateway, SCADA, historian
02
Execution
MES, manufacturing operations (MOM), SAP ERP
03
Data platform
Lakehouse, semantic layer, an ontology of machines, orders, batches and materials
04
Applications
Digital twin, machine-learning forecasts, dashboards, agents
The controls
Autonomy, inside the rules of the plant.It can act. It can’t go rogue.
The same rules I write into an agent’s job description, built into the console, so you can see them work.
Two-person approval
Safety-relevant actions, such as stopping a machine or holding a lot or an order, wait for a second person. The approval is recorded.
Roles
Operator, engineer, plant manager and executive each see their own view. Every switch between roles is logged.
Audit log
Every system event, user action and agent action is recorded with time, actor, action and outcome.
Autopilot, with limits
Closed-loop recovery restores failed systems, connectors and machines on its own. Safety and AI actions still need a person.
OT security
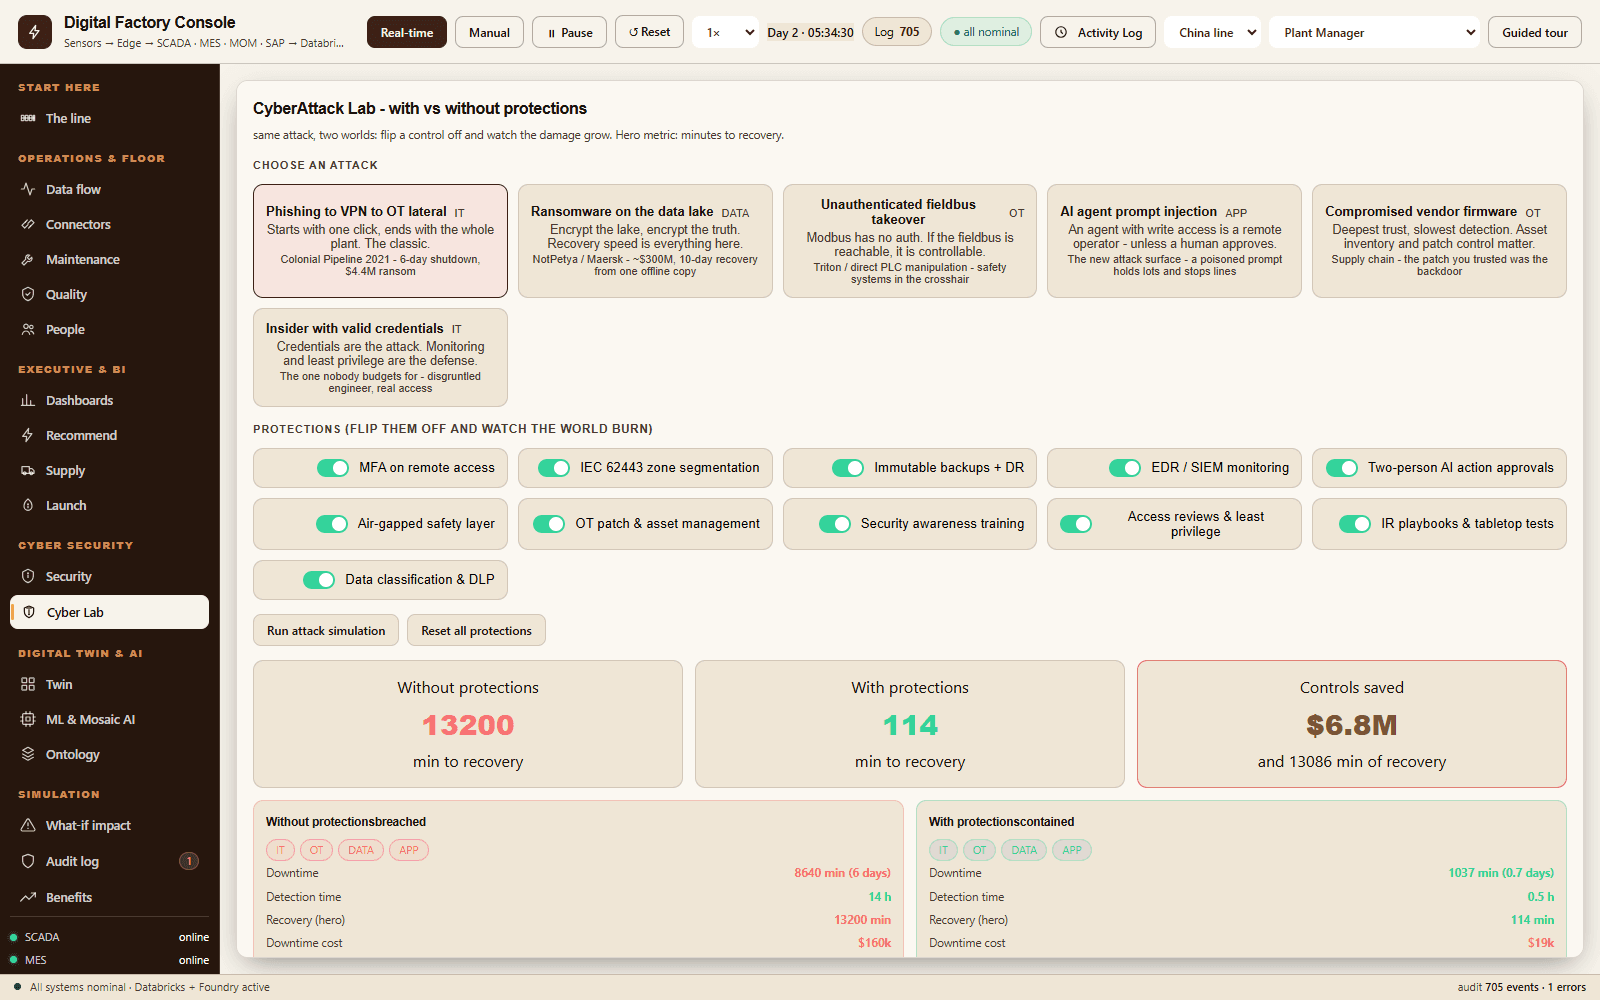
IEC 62443 zones from field devices to enterprise IT, and an attack lab with six scenarios, including prompt injection against an AI agent, run with and without protections.
Inside the console
What you will seeScreenshots, for the skeptics
Screens from the live console, which is in English.
Today: the operator clears six alarms and the lot ships.With agents: one incident, a held lot, a second person to approve.The digital thread: switch any system off and watch the impact.The attack lab: the same attack, with and without protections.
Built from programs I have run.I’ve stood in this mud before.
The console is a demonstration. The patterns in it come from programs on my record.
Project Phoenix linked SAP S/4HANA, IIoT, MES and digital twins across 45+ production lines. OEE rose 32%, and the Suzhou factory joined the World Economic Forum’s Global Lighthouse Network.
Digit-AI took AI use cases from pilot to production, with a 17.2% efficiency improvement across an industrial group’s China business. The same program put plant-edge computer vision for quality control on the line at Tianjin.